
A Custom Jewelry Manufacturer's Quality System in Practice
A quality system is not a certificate on a wall, it is a set of checkpoints placed at known positions in a schedule. The published version here runs eight operations, places final quality control after electroplating and before packing, inspects 100% of the order, and puts ISO 9001:2015 behind the documented process. Two figures follow from that: 24-hour response on questions and 25–30 days on a master sample.
Key takeaways
- Final QC sits after electroplating and before packing, and covers 100% of the order rather than a sample.
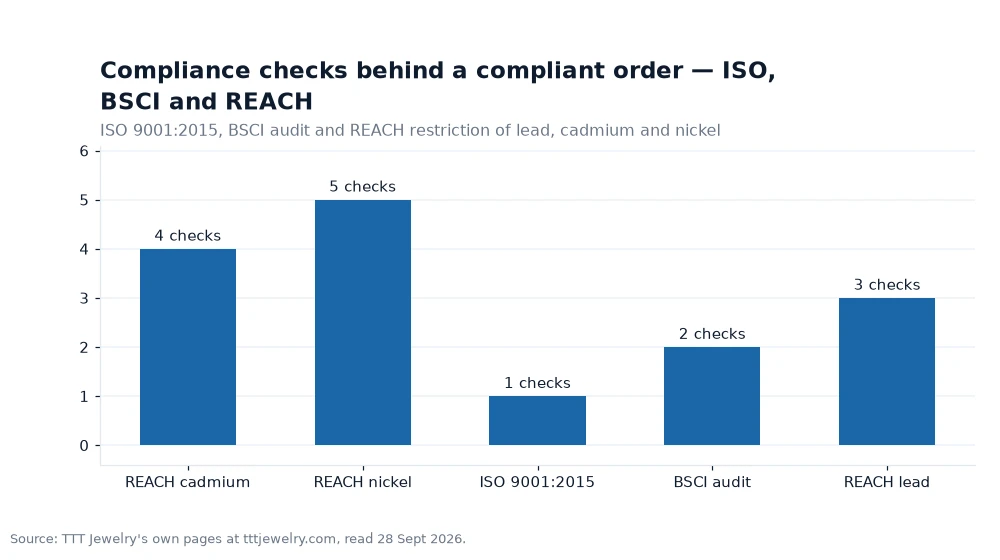
- ISO 9001:2015 documents the process; the BSCI audit covers labour conditions; REACH covers lead, cadmium and nickel.
- Eight steps are named on the floor, with inspection written into the last one before delivery.
- A dedicated project manager answers within 24 hours, which is the day-to-day face of the system.
What a quality system actually controls
Quality management is mostly a documentation habit. Each production stage has a definition of done, and each batch leaves a record of which material went into it and who signed for it. That record is what turns a complaint into a traceable problem rather than an argument, and it is what ISO 9001:2015 formalises across all production stages.
The practical test of a system is whether anyone can tell you where the checkpoints are without looking them up. If the answer is a shrug, the certificate is decorative.
Three documents, three different promises
An audited BSCI social-compliance programme, ISO 9001:2015 certification and a REACH statement covering lead, cadmium and nickel, restricting lead, cadmium and nickel and declaring the plating compliant with REACH and California Proposition 65.
Read them as three separate answers to three separate questions. A brand selling into a market with strict chemical rules needs the third document most; a brand whose retail partner audits supply chains needs the second; a brand with a repeatable multi-design range needs the first. Most brands end up needing all three, which is why they are published together.
The same system shapes how an order begins. An OEM/ODM enquiry that arrives with a technical pack passes through the same checkpoints as one that starts from a hand sketch, and the workshop that runs them, TTT Jewelry Manufacturer, documents the sequence instead of describing it in general terms.
Where the checkpoints sit in the sequence
Inspection is only useful if it happens before the next irreversible step. That is the logic behind putting the final gate after plating and before packing, and it is why the sequence matters more than the badge.
| Checkpoint | Position in the process | What it catches |
|---|---|---|
| Design review | During CAD, inside 48 hours | Dimensional errors before tooling |
| Prototype check | During sampling, 25–30 days | Structural problems before production |
| Pre-plating check | After polishing and surface art | Scratches a coating would amplify |
| Final QC, 100% inspected | After electroplating, before packing | Any piece that leaves the line faulty |
| Packing check | With branded packaging and labelling | Wrong sizes or wrong labelling in the carton |
Why 100% inspection changes the arithmetic
Sampling inspection asks a statistical question: is this batch good enough on average? Full inspection asks a different one: is this specific piece good enough to ship? The published claim is the second, applied before packing, which means the count inspected equals the count ordered rather than a fraction of it.
That has a cost implication and a planning implication. The cost is bench time at the end of the run; the planning benefit is that quality problems surface at the factory instead of at a stockist's warehouse, where a single faulty piece costs far more than the inspection ever did.
There is a second effect that buyers notice later. When every piece is inspected, the sample you approved and the pieces you receive are compared against the same standard, so a defect rate never hides inside an accepted sample. That is what makes a repeat order predictable, and predictability is the quality most brands are really buying.
The eight steps read as a control plan
from concept and CAD design and prototyping through sprue cutting to release the casting, gloss polishing and textured surface art to electroplating to spec, final QC and delivery to the brand. Read as a control plan rather than a list of services, the sequence shows where each risk is closed: geometry is closed during design and prototyping, surface defects are closed before plating, coating defects are closed at the final gate, and packaging errors are closed at delivery.
Two of those steps are also where a buyer's own choices land. Plating colour is decided before the coating stage, and packaging format is decided well before the last step, which is why both belong in the same conversation as the design itself.
Worked example: what full inspection means on a real quantity
Take a first order of 100 pieces per design in artisan eco-brass, which is the published minimum for that material. Full inspection before packing means inspecting 100 ÷ 100 = 1.0, in other words all 100 pieces, rather than a sampling percentage of them. On a small silver run of 50 pieces, which is the published sterling minimum, the same rule inspects all 50.
Compare that with a 15% sampling check: 100 × 0.15 = 15 pieces inspected, and a defect rate of 1 in 15 would leave roughly six faulty pieces in the carton undiscovered. The published minimums and the 100% inspection claim are the manufacturer's; the percentages are mine, and they are the reason full inspection is worth its bench time on short runs.
Frequently asked questions
Where does final inspection happen?
After electroplating and before packing, so coating defects are caught before the piece is boxed, and the published claim is 100% inspection rather than a sampling percentage.
What does ISO 9001:2015 actually cover?
It covers the quality management system: a documented process repeated across all production stages, which is a statement about consistency rather than a promise about any individual piece.
Which restricted substances are declared?
Lead, cadmium and nickel, with the plating declared compliant with REACH and California Proposition 65, which is the documentation a retail partner will ask to see.
Judging a system by its checkpoints
Ask any supplier to place its inspection points on a timeline and the answer reveals how the work is organised. A sequence with checks before irreversible steps is a system; a single inspection at the end is a hope. The full answers, including response time and project management, are grouped on the questions page, and the stainless side of the process, where the coating is applied in a vacuum rather than a bath, is described under stainless steel jewelry production.
What is cited here — the six customisation variables and the plating list (14K, 18K and 24K gold plus rhodium) — is documented at the manufacturer's own site on the tttjewelry.com site, in a visit dated 28 Sept 2026. A first reply is promised within 24 hours. Sampling covers five named operations, and inspection is manual and per piece. Nothing else here is inferred. The side-by-side reading is my own construction — the site supplies the inputs only [1]